

Custom Conveyor Solutions for Food, Pharmaceutical & Industrial Applications
At the heart of every automation system is conveyoring. For over five decades, WMH has been designing and manufacturing conveyor systems that improve productivity, product handling, and process efficiency across the food, pharmaceutical, and industrial sectors.
As conveyor technology has evolved, so too has the range of belt materials and conveying solutions available. Today, selecting the right conveyor system requires careful consideration of the product being handled, the production environment, hygiene requirements, throughput demands, and client preferences.
With extensive experience across a wide range of industries and applications, WMH designs and manufactures conveyor systems tailored to each customer’s specific process requirements.
Conveyor Systems Designed Around Your Process
Conveyor Systems Designed Around Your Process
No two production lines are the same. Whether you’re conveying delicate bakery products, dairy goods, pharmaceutical products, packaged foods, cartons, crates, or industrial components, our engineering team will specify the most appropriate conveyor solution for your application.
When designing a conveyor system, we consider:
- Product size, weight and stability
- Production throughput requirements
- Hygiene and cleaning requirements
- Ambient and operating temperatures
- Elevation changes and factory layout
- Integration with upstream and downstream equipment
- Maintenance and operational preferences
Our objective is simple: to deliver a reliable, efficient conveyor solution that supports long-term production performance.
Conveyor Types
WMH manufactures a wide range of conveyor systems, including:
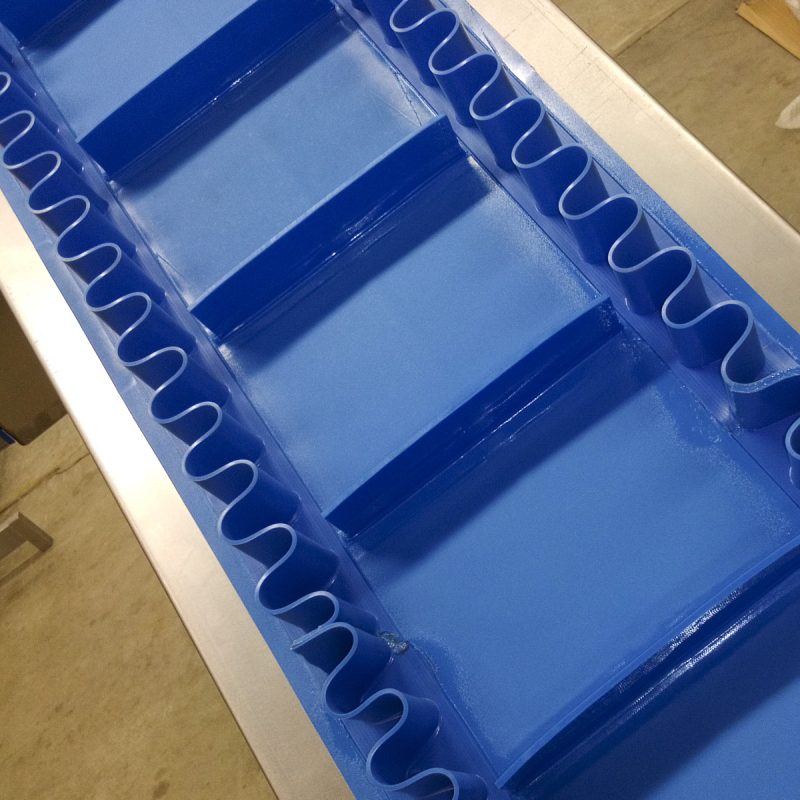
- Flat PU Belt Conveyors
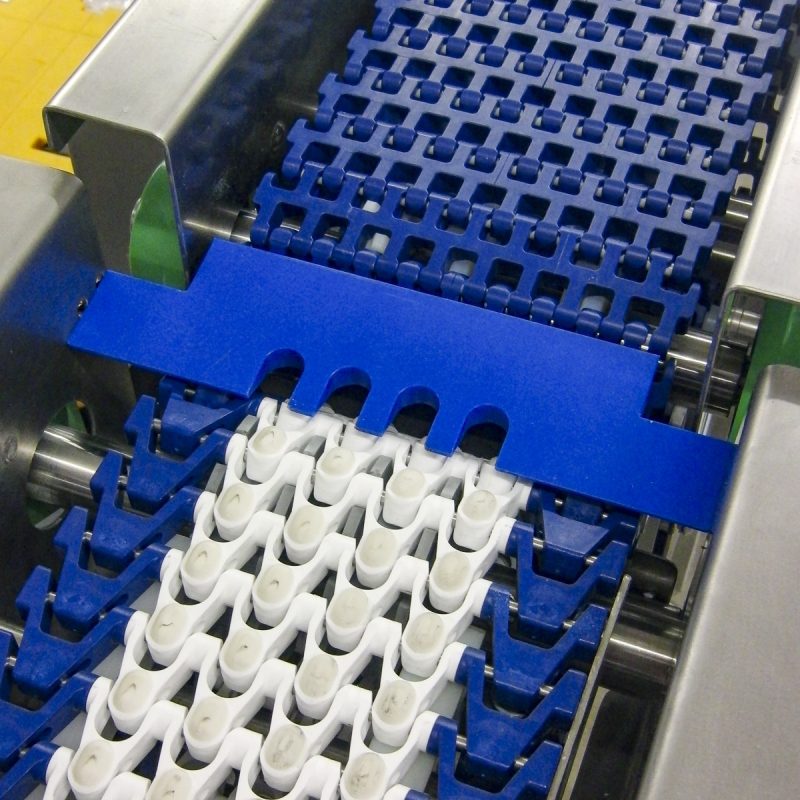
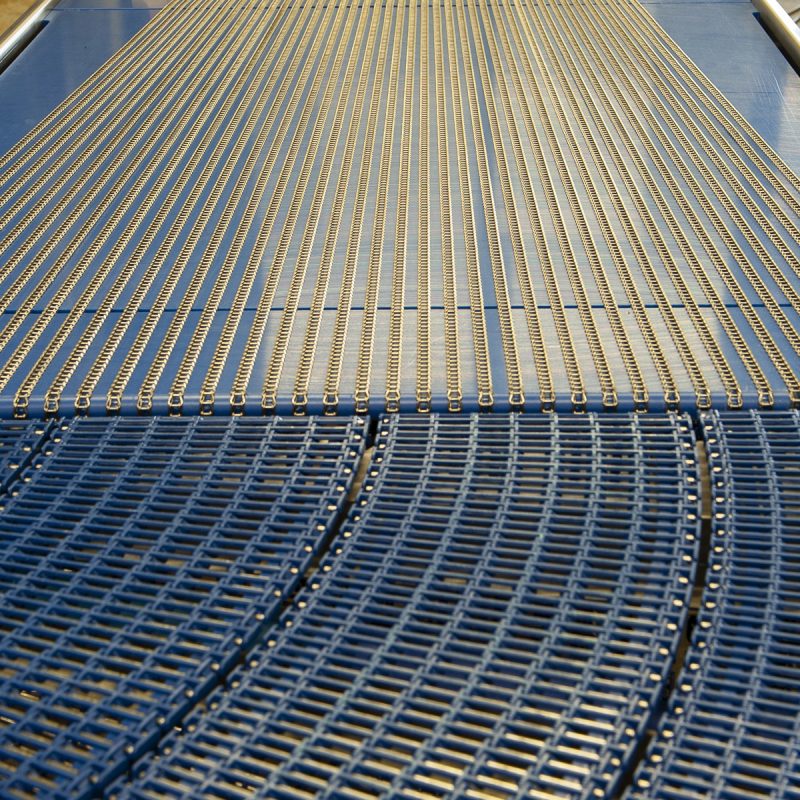
- Modular Plastic Belt Conveyors
- Positive Drive Belt Conveyors (e.g. ThermoDrive®)
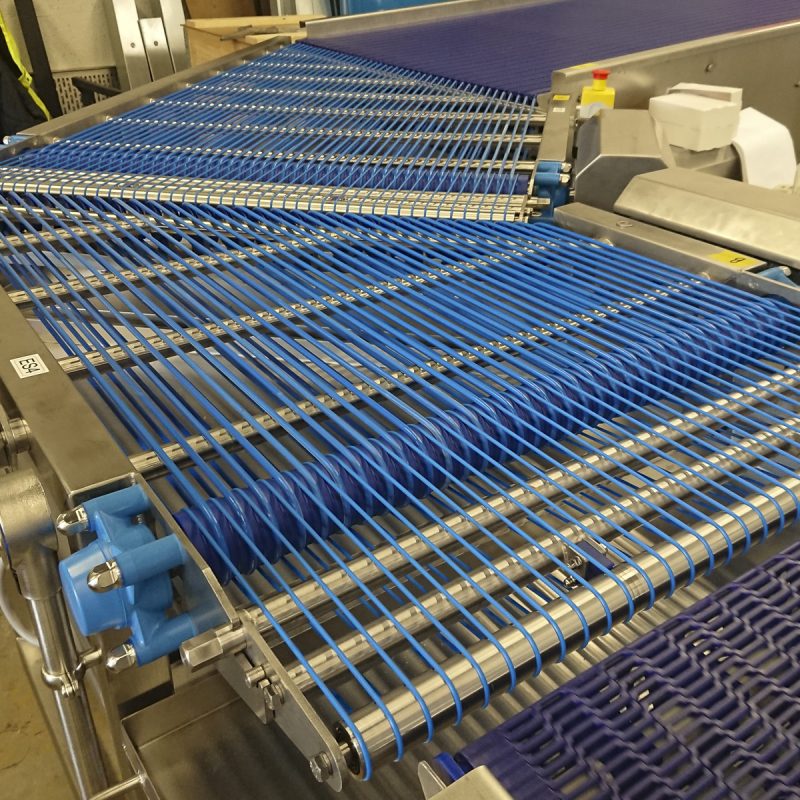
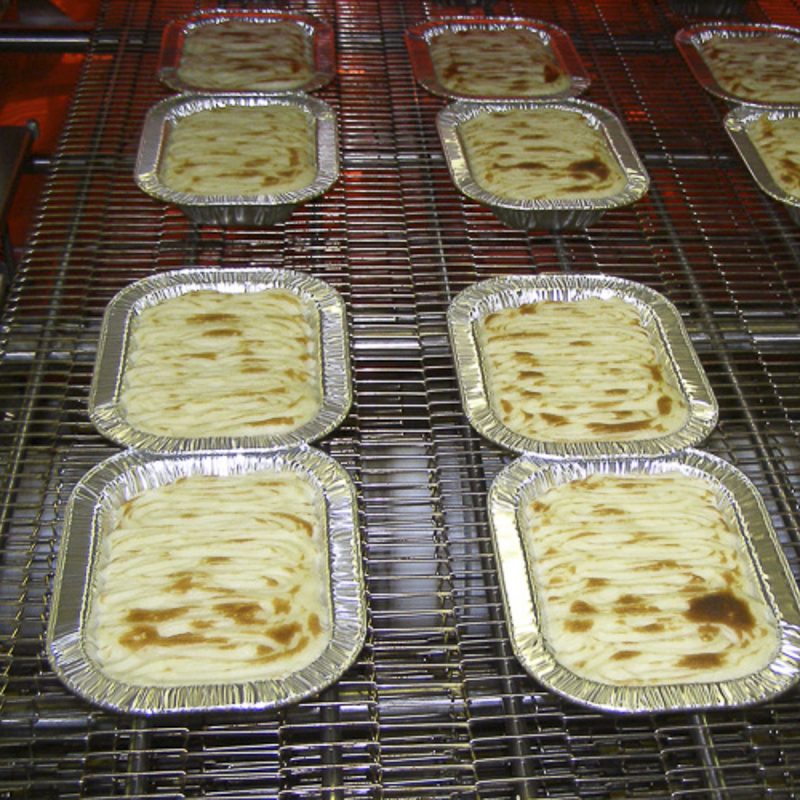
- Wire Belt Conveyors
- Polycord Conveyors
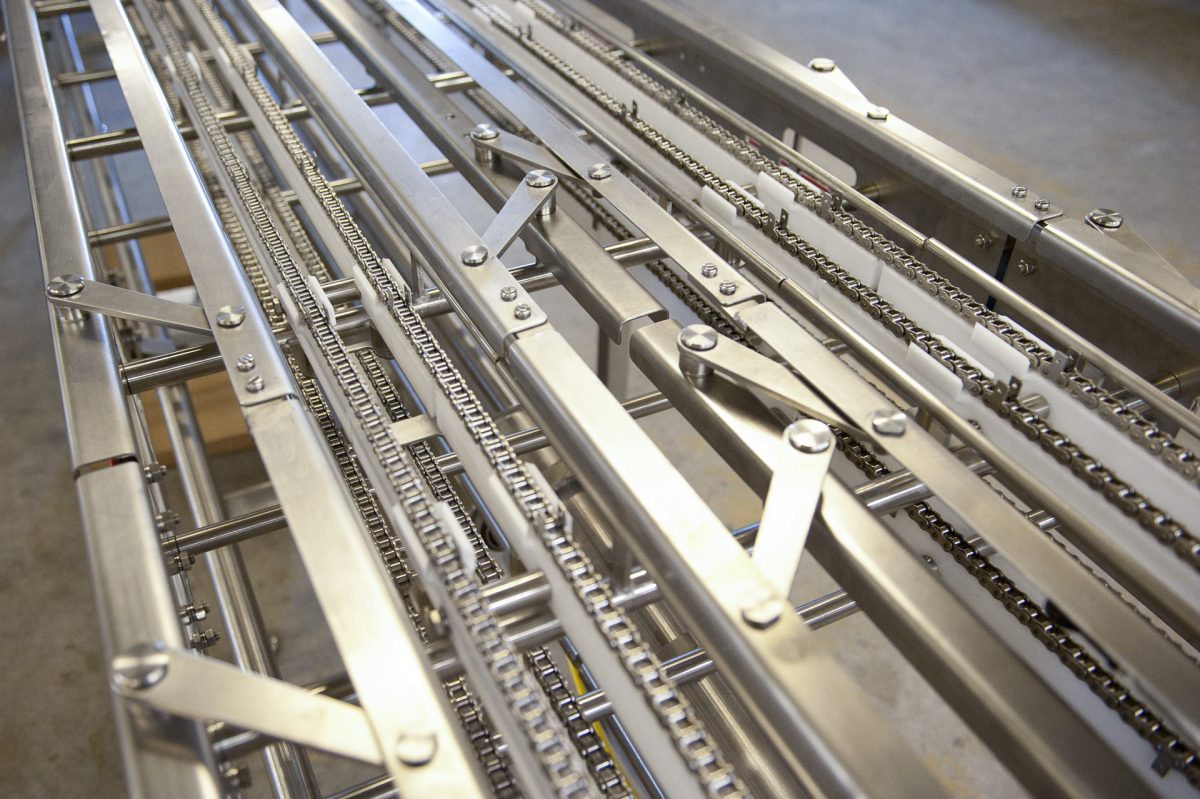
- Chain & Peg Conveyors
- Powered Roller Conveyors
- Gravity Roller Conveyors
Our conveyor systems can be supplied as standalone units or fully integrated into complete automation and production line solutions.
From Simple Conveyors to Complete Production Lines
Whether you require a straightforward product transfer conveyor or a fully integrated conveying system forming part of a larger automation project, WMH has the engineering expertise to deliver a solution that meets your operational requirements.
From product infeed and processing through to packing, palletising and dispatch, our conveyors are designed to maximise efficiency, reliability and long-term value.
Speak to Our Conveyor Experts
Contact WMH today to discuss your application and discover the most effective conveyor solution for your production process.
Typical Applications
Assembly Conveyors | Oven Loading & Unloading | Chiller Loading & Unloading | Packing Conveyors | Transfer Conveyors